Box Column Electroslag Welding Equipment in India: Hualian's Integrated Box-Beam Fabrication Systems
Sep 29, 2026
Wuxi, Jiangsu Sep 29, 2026 (Issuewire.com) - Fabricating heavy structural box columns for high-rise commercial towers, metro rail viaducts, and industrial plants across India requires advanced electroslag welding technology. Specializing in heavy structural and electroslag joining systems since 1987, Wuxi Hualian Science & Technology Group--known across global steel construction markets as Hualian, delivers dedicated electroslag welding machines engineered specifically for internal box-column diaphragm joining. Internal diaphragm plates provide essential multi-axis stiffness, transferring massive beam moments into vertical columns. Traditional manual welding methods cannot access restricted interior diaphragms once box column plates are enclosed. Consumable-guide electroslag welding provides an automated joining solution engineered specifically for blind interior joints.
Electroslag welding changes from an arc to resistance heating
Although frequently grouped with automated arc processes, electroslag welding undergoes a fundamental transformation during operation. The process begins with an electric arc striking inside a small sump at the joint bottom beneath granular conductive flux. As flux melts, a deep molten slag pool develops. Once the conductive slag pool reaches approximately 30 mm to 40 mm in depth, the electric arc extinguishes completely. Welding current then flows directly from the consumable guide tube and wire electrode through the molten slag into the base metal. Electrical resistance within the molten slag pool generates intense heat, maintaining temperatures between 1,600°C and 1,800°C.
This uniform resistance heat progressively melts the consumable guide tube, filler wire, and joint sidewalls, creating a dense, defect-free weld pool without arc spatter. Because the process operates by resistance heating rather than an electric arc, magnetic arc blow is completely eliminated, ensuring stable deposition across deep joint cavities. Maintaining steady slag bath depth prevents arcing instabilities, producing uniform metallurgical fusion along the entire vertical joint depth. Monitoring electrical current and voltage stability during slag pool formation ensures smooth transition from arc to resistance heating. Digital current meters detect fluctuations instantly, allowing operators to adjust wire feed rates and stabilize the molten bath.
The internal connection defines the equipment problem
Welding internal diaphragms within heavy box columns presents a severe geometric challenge. Once three column plates are assembled, access to the interior joint is restricted to small holes drilled through the outer column plates. Conventional welding torches cannot access internal corners. Consumable-guide electroslag welding solves this physical obstruction. A flux-coated steel tube carrying the filler wire extends vertically through the outer access hole down into the diaphragm joint cavity. The stationary guide tube melts progressively as the weld pool rises vertically from bottom to top in a single continuous pass. This eliminates the need for traveling carriage mechanisms inside the enclosed steel box.
Water-cooled copper backing shoes clamped outside the access holes contain the liquid slag and molten steel pool, creating smooth, flush weld faces. Solidified copper-backed weld surfaces require minimal cosmetic grinding, accelerating downline column transit into external submerged arc welding gantries. Because electroslag welding proceeds without visual inspection of the internal cavity, water-cooled copper retaining shoes must seal access holes tightly. Pneumatic clamping bars hold the copper shoes firmly against the outer plate faces, preventing liquid slag leakage. Reliable slag containment maintains uniform resistance heating throughout the vertical weld progression.
Equipment selection and joint qualification answer different questions
Equipment selection focuses on machine rigidity, electrical power source duty cycle, wire feeding precision, and vertical clamping clearance. Hualian manufactures cantilever DZ-1200X and portal MDZ-1200 electroslag welders engineered for structural steel column lines. However, possessing advanced machinery does not automatically satisfy building codes like AWS D1.1. Structural joints require formal procedure qualification. Because electroslag welding involves high heat input and slow cooling rates, grain growth occurs in the heat-affected zone. Fabricators must select specialized flux formulations, control welding voltage between 38V and 45V, and verify impact toughness through Charpy V-notch testing on representative test plates.
Establishing qualified welding procedure specifications guarantees that heavy diaphragm joints achieve the ductility and fracture toughness required in seismic building zones. Controlling heat input through regulated wire feeding speeds limits heat-affected zone coarsening, preserving base steel toughness. Electroslag welding procedures must specify precise consumable guide tube wall thicknesses and flux coating formulations. Uniform guide tube melting prevents un-melted steel fragments from dropping into the liquid weld pool, eliminating internal metallic inclusions.
Match the equipment arrangement to the fabrication duty
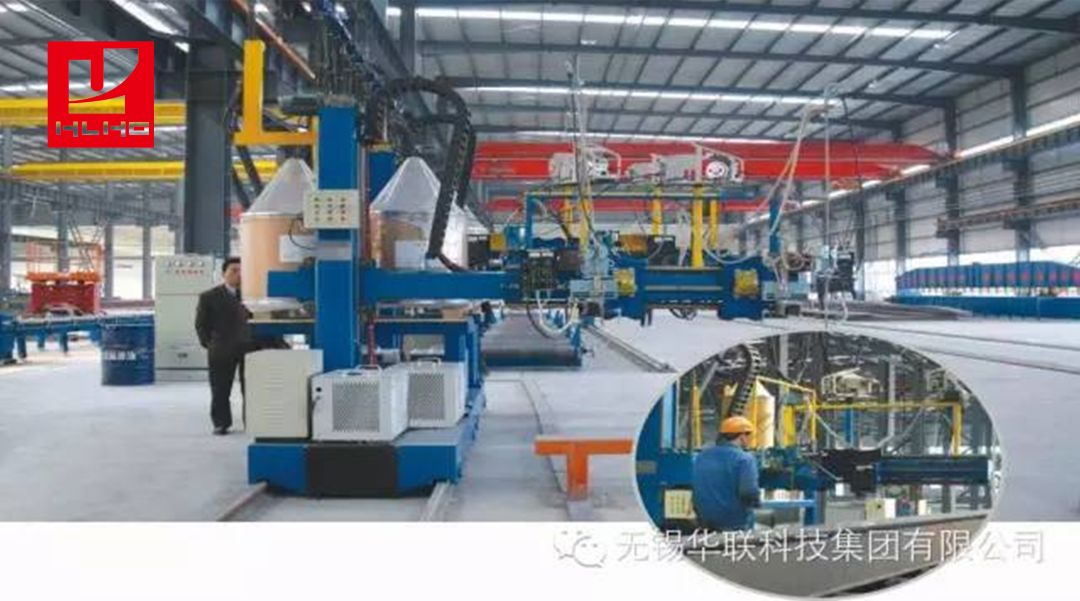
Workshops in India must select electroslag machine frames that suit column dimensions and workshop handling methods. Cantilever electroslag welders feature an outstretched boom mounted to a single vertical column. The open-sided frame provides unrestricted overhead crane access, simplifying the loading and unloading of non-standard box sections. For high-volume column fabrication, portal gantry frames straddle two parallel welding beds, allowing operators to set up one column while welding continues on the adjacent bed. Selecting the appropriate machine layout balances capital investment with shop floor material handling capacity. Dual-bay portal machines maximize power source utilization, enabling operators to weld two diaphragms simultaneously on opposite column sides. Cantilever welding booms feature motorized vertical elevation drives with precision brake motors, preventing accidental carriage dropping during setup. Counterweighted slide mechanisms allow smooth manual positioning when inserting consumable guide tubes into plate access holes.
Address the thermal and mechanical requirements of the joint
Electroslag welding thick diaphragm plates ranging from 40 mm to 80 mm demands strict thermal management. Steel plates must be preheated to specified interpass temperatures to prevent thermal shock and cold cracking. Because the diaphragm joint is visually inaccessible inside the enclosed box, non-destructive testing requires rigorous ultrasonic examination. Technicians must conduct angle-beam ultrasonic testing through external column plates to verify complete side-wall fusion and detect any slag entrapment. Calibrating ultrasonic scanning angles and DAC curves against representative calibration blocks ensures reliable defect detection inside blind box column joints.
Specialized low-hydrogen flux formulations minimize diffusible hydrogen content in the solidifying weld pool, preventing delayed cold cracking in heavy structural column sections. Post-weld insulation blankets placed over the access holes slow cooling rates, helping relieve localized residual stresses across thick diaphragm joints. Angle-beam ultrasonic testing probes scan the joint from multiple plate surfaces to verify complete fusion along diaphragm edges. Calibrating ultrasonic instruments against certified test blocks guarantees defect detection in thick column assemblies.
Build an India equipment inquiry around the joint dossier
Indian EPC contractors and structural steel fabricators planning to procure electroslag equipment should assemble a comprehensive project inquiry. Sizing welding power sources and guide tube lengths around actual column cross-sections prevents costly field modifications. Detailed inquiries should include column wall thicknesses, diaphragm plate schedules, steel grades, and monthly production volumes.
Engineering managers in India can consult Hualian to evaluate customized electroslag welding systems, transformer power ratings, and workshop integration layouts: https://www.hualianoversea.com/. Hualian delivers integrated box-beam manufacturing machinery engineered for demanding structural fabrication projects.
Source :Wuxi Hualian Science & Technology Group
This article was originally published by IssueWire. Read the original article here.
YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.


